Outlook: Automation in High-Speed Post Press Finishing Lines
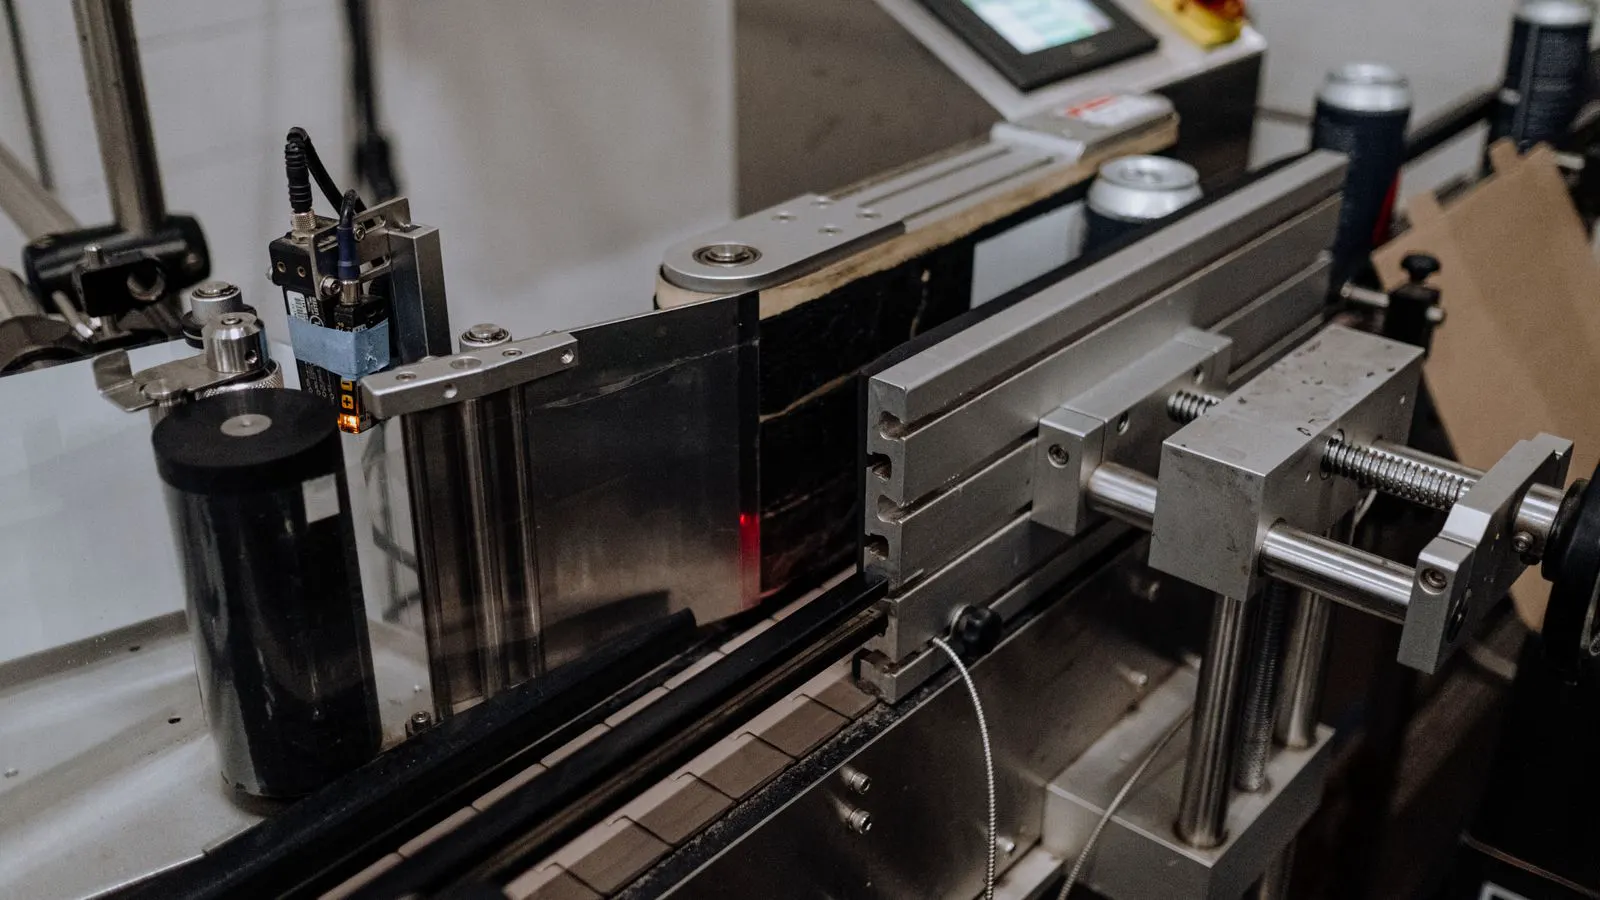
High-speed post press automation shifts work from manual stations to automated lines. Buyers should plan for better throughput, lower finishing labor costs, and new maintenance demands. This outlook covers five shifts to prepare for.
- Post press automation moves high-volume work from manual labor to controlled mechanical systems.
- Finishing labor costs drop when operators manage multiple machines rather than performing repetitive tasks.
- Production efficiency improves through synchronized feeds and automated quality checks.
- Preparation requires retraining staff, updating maintenance routines, and verifying line integration.
- Buyers should focus on throughput capacity, service support, and workflow compatibility before purchasing.
What changes when you replace manual stations with automated lines
High-speed post press automation changes the daily rhythm of a print shop. Manual folding, gluing, and trimming stations often rely on steady hand speed and visual checks. Automated lines replace those repetitive motions with motorized feeds, sensor-guided registration, and continuous transport. The operator no longer stacks, flips, and passes sheets through a single station. Instead, the operator monitors multiple machines at once.
The shift is not simply about speed. It changes how work is planned, how defects are caught, and how labor is distributed across the day. A shop that once needed six people at the finishing line may run the same volume with two or three operators who manage the line, handle exceptions, and perform quality checks. This change directly affects finishing labor costs and production efficiency.
Automation also changes the nature of errors. Human fatigue causes slow drift in registration and inconsistent glue application. Automated systems maintain tighter tolerances but fail in different ways. A sensor misread, a jam, or a software glitch can stop the line. The cost of a failure shifts from a few bad units to a full production stoppage. This requires a different mindset for setup and troubleshooting.
How finishing labor costs shift with automation
The most visible benefit is the reduction in manual labor hours. When a line folds, binds, and trims in one continuous flow, operators spend less time on repetitive tasks. They spend more time on machine monitoring, setup, and problem solving. The labor profile changes from high-volume manual work to lower-volume supervisory work.
Finishing labor costs do not disappear. They move. The shop may need fewer operators per shift, but it needs more skilled ones. The same people who once folded and glued now need to read error codes, adjust feed guides, and manage material changes. Training becomes a recurring cost, not a one-time expense.
There is also a trade-off in flexibility. Manual stations can handle small runs with quick manual adjustments. Automated lines often require minimum run lengths to justify setup time. A shop that prints many short runs may keep some manual stations for short jobs and use automation for high-volume work. The cost calculation must include changeover time, not just unit labor time.
How production efficiency improves through synchronized flow
Production efficiency gains come from removing handoffs. In a manual line, sheets pass from one person to another. Each handoff creates a pause, a potential misalignment, and a chance for a drop. Automated lines eliminate these pauses. Sheets move on conveyors, and sensors track registration and material position.
The line operates as a single unit. If the trimmer stops, the feeder slows or stops. If the binder detects a glue error, the system flags the unit. This synchronization creates a clear signal of where problems occur. Operators can isolate issues quickly instead of guessing which station caused a batch of bad sheets.
Efficiency also improves in material handling. Automated lines often use flatbed or vertical infeed systems that load large quantities of stock. Operators load a pallet or a large stack and the line pulls sheets as needed. This reduces the need to carry sheets by hand and lowers the risk of damage. The floor becomes less crowded and safer.
What buyers should plan for in the first year
The first year of operation is the most critical period. The line will reveal workflow gaps that were hidden when the shop ran manual stations. Buyers should expect a period of adjustment. The plan should cover training, maintenance, and workflow redesign.
Training is the first priority. Operators need hands-on time with the machine before production runs. They should learn how to load stock, set guides, run a short test batch, and interpret error messages. A common mistake is sending an experienced manual worker to run the line without proper training. The worker knows the print job but not the machine.
Maintenance planning is the second priority. Automated lines have more moving parts and electronic components than a manual station. Filters, belts, bearings, and sensors require regular attention. The shop should build a maintenance schedule into the daily workflow. A small preventive check can prevent a full line stop.
Workflow redesign is the third priority. The shop needs to decide which jobs go to the automated line and which stay manual. Short runs, odd sizes, and special finishes may not fit the automated line. The plan should define clear rules for job assignment. Without clear rules, operators may overload the line or underutilize it.
How to prepare the floor and workflow for automation
The floor layout needs review before the line arrives. Automated finishing lines require space for infeed, machine body, outfeed, and finished goods staging. The space must allow safe access for maintenance and material handling.
The workflow needs to change from batch-based to line-based. In a manual setup, jobs are often completed at one station at a time. In an automated setup, the line runs continuously, and jobs are queued. The shop needs a way to manage that queue. A simple digital board or a basic scheduling tool can help.
Quality checks need redefinition. In a manual line, the operator inspects sheets by hand. In an automated line, the system performs checks, but the operator must verify the system. The shop should set a clear inspection point after the line, where a sample is checked against the proof. This prevents bad sheets from reaching the customer.
A practical comparison of manual and automated finishing
The difference between manual and automated finishing is best shown by comparing the work steps. The table below shows how each step changes when the line is automated.
| Work Step | Manual Station Approach | Automated Line Approach |
|---|---|---|
| Infeed | Operator loads and feeds sheets by hand | Motorized feeder pulls sheets from a stack |
| Folding | Operator folds and passes sheets | Mechanical folder folds at set angle and speed |
| Binding | Operator applies glue or uses a manual binder | Automatic binder applies glue and presses at set time |
| Trimming | Operator loads and trims sheets in batches | Trimmer cuts at set dimensions with continuous feed |
| Quality Check | Operator inspects by eye and hand | Sensors check registration and flags defects |
| Labor Role | Repetitive manual work | Monitoring, setup, and exception handling |
This comparison shows that automation does not remove the work. It changes the work. The physical tasks are reduced, but the cognitive tasks increase. The operator must understand the machine, the material, and the quality standards at the same time.
How to evaluate a line before you buy
Buyers should evaluate a finishing line on five factors. The first is throughput capacity. The line must handle the expected volume without becoming a bottleneck. If the line can handle 5000 sheets per hour, but the shop only needs 2000, the extra capacity may not be worth the cost.
The second is setup time. A line that takes 30 minutes to change over between jobs may not be as efficient as a line that takes 10 minutes. Setup time adds up over the day and affects production efficiency.
The third is service support. The shop needs a reliable service partner who can respond quickly. A line that breaks down for a day can lose a full day of production. The service agreement should be part of the purchase decision.
The fourth is workflow compatibility. The line should fit the existing floor and the existing job mix. If the line requires a complete floor redesign, the cost and disruption may not be justified.
The fifth is operator readiness. The shop should assess whether the current staff can be trained for the new role. If not, the shop may need to hire or reassign staff before the line arrives.
What this means for the next few years
The direction is clear. More print shops are moving high-volume finishing work to automated lines. The reason is not only speed. It is the combination of lower finishing labor costs, tighter quality control, and better production efficiency. The manual station will not disappear. It will remain for short runs and special jobs. But the high-volume work will increasingly move to automation.
Buyers who prepare now will be in a better position than those who wait. The preparation is not complicated. It involves understanding the machine, training the staff, and adjusting the workflow. The cost of preparation is small compared to the cost of a poorly run line. The goal is a line that runs smoothly, produces consistent work, and frees the team to focus on quality and customer service.
Frequently asked questions
How much labor can post press automation reduce?
Automation can reduce manual labor hours significantly by replacing repetitive tasks with machine operation. The exact reduction depends on run size and job complexity.
Does automation require a larger floor space?
It depends on the line size and layout. Buyers should measure the infeed and outfeed space before purchasing a line.
Can a shop run short jobs on an automated line?
Short jobs may not be as efficient on an automated line due to setup time. Many shops keep manual stations for short runs and use automation for high-volume work.
What is the biggest mistake in post press automation setup?
The biggest mistake is underestimating training and maintenance. Operators need hands-on training, and the line needs a regular maintenance schedule.
How do I know if my shop is ready for automation?
A shop is ready when it has a clear job mix, trained staff, and a maintenance plan. The shop should also have the floor space and workflow structure to support the line.